Accordian Closable

7 Tips for Buying Automated Welding Cells?

Buying automated welding cells is not simply a robotics purchase. It is a production decision involving labor, safety, quality, maintenance, and future product changes. A cell may look impressive under showroom lighting, yet struggle with your actual fixtures, weld access, or material variation.

The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023, with global operational stock exceeding four million units. These figures show strong automation demand, but they do not guarantee a successful welding project. The right system depends on arc quality, cycle time, operator skill, part presentation, and integration capability. Fit matters.

This guide presents seven practical tips for evaluating automated welding cells. It considers robot reach, power-source compatibility, positioners, sensing, programming, guarding, service support, and total ownership cost. OSHA guidance highlights risks involving unexpected startup and robot movement, while ISO 10218 provides an important reference for industrial robot safety. These standards should shape supplier discussions, not decorate a compliance folder.

Real factories also reveal uncomfortable details. A cell can meet its advertised cycle time with perfect parts, then lose productivity when fixtures need adjustment. A low purchase price can become expensive through downtime, spare-part delays, or difficult programming. The numbers help. They are not the whole answer.

Before comparing quotations, record your real weld lengths, part weights, joint tolerances, changeover frequency, and operator concerns. Ask suppliers to demonstrate representative parts, not generic samples. Reports provide industry context; hands-on trials provide evidence. That gap matters. A careful buyer should challenge assumptions, document limitations, and leave room for improvement after installation.
7 Tips for Buying Automated Welding Cells?

Map Part Volume, Weld Length, and a 50–70% Target Arc-On Time

Buying an automated welding cell starts with the part, not the robot. Map annual part volume, batch size, material, and fixture changes. Then measure weld length for every joint. A 400-millimeter seam behaves differently from eight short stitches. Record loading, clamping, repositioning, and inspection times. Small delays often control the cell’s real capacity.

Set a realistic arc-on target between 50% and 70% of available production time. Arc-on time means the torch is actively welding. It does not include waiting, movement, or operator loading. Calculate required hours from total weld length, travel speed, starts, stops, and rework. Include peak-month demand, not only the yearly average. Peaks expose weak planning.

Choose a cell that can handle your largest practical assembly, while protecting access and torch angles. Check fixture repeatability, fume extraction, programming access, and maintenance space. Ask for a time study using your parts. Request proof with representative welds, not a polished demonstration piece. My early estimates were too optimistic because I ignored fixture cleaning. That mistake still matters. Leave room for skill differences, wire changes, and occasional troubleshooting. A cell running at 90% arc-on time may look efficient, but it has little recovery space. Seven useful checks are simple: measure, calculate, test, observe, question, document, and review. Each one can change the purchase decision.

7 Tips for Buying Automated Welding Cells

Map part volume, weld length, and target a practical arc-on time of 50–70% before selecting cell size, robot reach, positioner capacity, and material-handling equipment.

This planning model compares low-, medium-, and high-volume production profiles. Higher daily volume and longer weld length generally justify greater automation capacity, while the 50–70% arc-on range leaves time for loading, fixturing, repositioning, inspection, and changeovers.

Match Robot Reach, Payload, and Positioner Capacity to the Largest Part

7 Tips for Buying Automated Welding Cells

Match the robot’s reach, payload, and positioner capacity to your largest part. This sounds obvious. It is often missed. Measure the complete part envelope, including clamps, fixtures, and temporary supports. A robot may reach the joint but still lose access when the torch angle changes.

Check seven practical points before approving a cell. Confirm the robot can reach every weld without stretching near its limits. Verify payload calculations include the torch, cable package, sensors, and tooling. Size the positioner for the part’s weight, center of gravity, and rotation speed. Inspect fixture clearance at every planned orientation. Test cable routing around sharp movements. Review welding samples using the actual material and joint design. Leave capacity for future parts.

In production reviews, I have found that fixture weight is regularly underestimated. One large frame looked manageable until its clamps shifted the center of gravity. The positioner then required slower motion, reducing output. That assumption was wrong. Ask for reach studies and load calculations, not only catalog ratings. Check working payload at the required extension, not at the robot’s ideal position. A simple full-scale mock-up can reveal collisions that software misses. It also exposes awkward loading heights and poor operator access. Small details matter. The best cell is not the largest one. It is the one that handles the biggest part safely, repeatedly, and with measurable room for change.

Specify Process Stability, Wire Feed, and a 60% Minimum Duty Cycle

7 Tips for Buying Automated Welding Cells

Buying an automated welding cell should begin with process stability, not appearance or advertised speed. Watch a complete production cycle, including arc starts, stops, repositioning, and part changes. A stable cell should maintain consistent bead width, penetration, and torch alignment across repeated welds. Ask for recorded test results, not only polished sample parts.

Wire feeding deserves close inspection. Check the feeder’s response during acceleration, sharp starts, and long cable runs. Inconsistent feeding can create bird-nesting, uneven deposition, or sudden arc interruptions. Examine liner condition, drive-roll pressure, wire straightness, and access for routine cleaning. Small feeding problems become expensive when operators must stop the cell repeatedly. They often do.

Specify a minimum 60% duty cycle for the intended welding current and production schedule. This means the cell can weld for six minutes within a ten-minute period, under stated conditions. Confirm the rating at your actual amperage, wire size, material, and shielding gas. A higher advertised rating may apply only to lighter settings. Include cooling capacity, torch temperature, maintenance intervals, and recovery time in the evaluation. Leave practical margin above 60%; production rarely follows laboratory timing. I have seen promising cells lose output because fixture loading, wire changes, and inspection were ignored. Ask operators to test those interruptions before approval. Reliability lives there.

Verify Cell Safety Against ISO 10218 and PL d Category 3 Controls

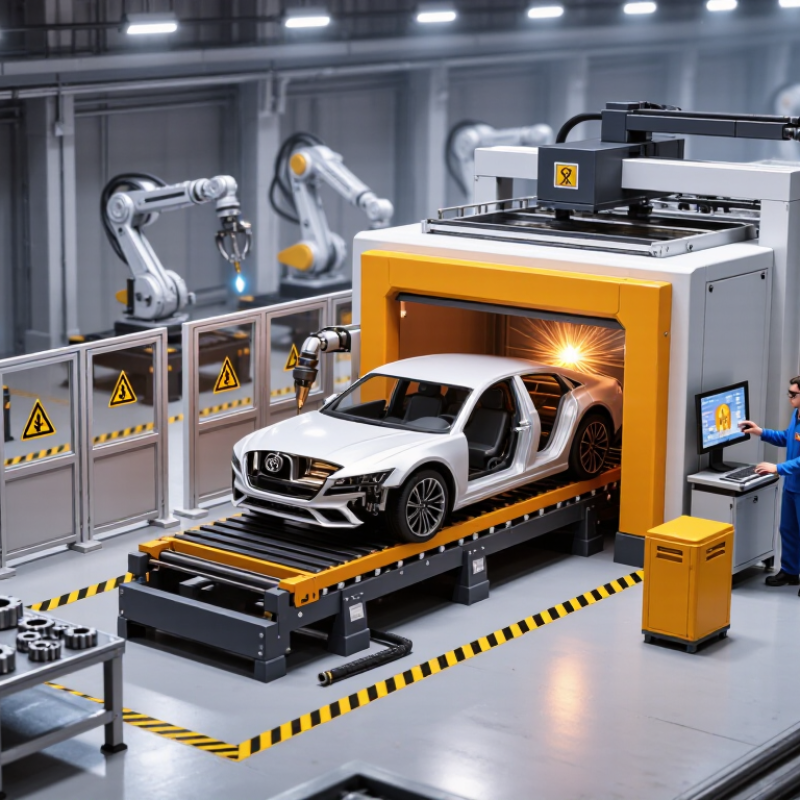
When buying an automated welding cell, treat safety verification as a purchasing requirement, not a final inspection task. Request the supplier’s risk assessment, safety circuit drawings, validation records, and operating instructions. Confirm that the design reflects ISO 10218 requirements for robot integration, guarding, access, teach modes, and emergency stops. A polished enclosure is not proof of safe control logic.

Examine every safety function separately. Door interlocks, light curtains, emergency stops, enabling devices, and reduced-speed modes should be identified clearly. Ask whether each function reaches PL d with Category 3 architecture, where a single fault should not cause loss of safety. The calculation should follow the applicable ISO 13849-1 method. Check diagnostic coverage, component reliability, and common-cause failure controls. Do not accept “PL d” as a label without test evidence.

Watch the cell operate. Open a guarded door and verify that hazardous motion stops before access is possible. Test restart prevention, reset location, trapped-person release, and fault indication. Ask an independent competent person to review the validation report. Small gaps matter. Welding fumes, hot fixtures, stored pneumatic energy, and unexpected restart require attention too. One practical weakness is often overlooked: maintenance staff may use a different access routine than operators. Document that routine, train the people involved, and record any unresolved risk before signing the purchase agreement.

7 Tips for Buying Automated Welding Cells? - Verify Cell Safety Against ISO 10218 and PL d Category 3 Controls

No. Buying Tip Safety Dimension to Verify Applicable Safety Basis Objective Acceptance Evidence Example Acceptance Criterion
1 Define the complete safeguarded space Identify the robot, positioners, welding equipment, fixtures, gas systems, cable routes, maintenance access, loading points, and possible reach-through or access openings. ISO 10218 cell-integration principles; risk assessment under ISO 12100. Approved layout drawing showing the safeguarded perimeter, access points, residual risks, and all operating and maintenance zones. No unassessed access route, pinch point, hot-work exposure, or stored-energy hazard remains outside the documented risk assessment.
2 Check guard and gate performance Verify fixed guards, interlocked movable guards, gate hinges, latches, trapped-key features where required, and protection against bypass or defeat. ISO 10218 safeguarding requirements; ISO 14119 for interlocking devices; ISO 14120 for guards. Guard inspection record, gate-interlock test results, tamper-resistance review, and photographs of access points. Opening any required protective gate initiates the defined stop function before hazardous motion can continue or restart.
3 Require a documented PL d, Category 3 safety circuit Review emergency stops, gate switches, enabling devices, safety controllers, contactors, robot safety inputs, and reset logic as one complete safety function. ISO 13849-1: Performance Level d, Category 3 architecture; validation under ISO 13849-2. Safety-function specification, SISTEMA or equivalent calculation, wiring diagrams, component data, and validation report. A single fault must not lead to loss of the safety function, and reasonably practicable faults must be detected; the calculated result reaches at least PL d.
4 Measure stopping performance before setting distances Measure hazardous-motion stopping time and stopping distance for the robot, positioner, and other moving equipment under worst-case load and speed. ISO 13855 for positioning safeguards with respect to approach speeds; ISO 10218 protective-stop and safeguarding requirements. Calibrated measurement report identifying test speed, payload, tooling, stopping command, measured time, measured distance, and measurement uncertainty. The installed safety distance is calculated from measured system behavior and the applicable standard, rather than copied from a generic layout.
5 Separate personnel protection from process control Confirm that production sensors, PLC commands, cycle-start signals, and software permissions cannot replace safety-rated protective devices. ISO 10218 control-system and safeguarding principles; ISO 13849-1 safety-related control systems. I/O list distinguishing standard control signals from safety signals, safety logic review, and fault-injection test records. Loss, short circuit, disconnection, or stuck state of a standard process signal cannot by itself defeat the required personnel-protection function.
6 Validate welding-specific residual hazards Assess arc radiation, fumes, hot surfaces, sparks, fire risk, shielding gas, compressed gas, electrical energy, and unexpected wire or torch movement. ISO 10218 risk-reduction framework; applicable welding, electrical, fire, ventilation, and workplace regulations. Fume-control assessment, ventilation verification, arc-screen inspection, thermal-risk review, gas-line inspection, and electrical safety records. The cell prevents or controls exposure to arc flash, welding fumes, hot workpieces, gas-release hazards, and ignition sources during automatic and manual modes.
7 Make commissioning and periodic validation contractual Define factory acceptance testing, site acceptance testing, operator training, lockout procedures, safety-function validation, and change-control requirements. ISO 10218 documentation and integration expectations; ISO 13849-2 validation; ISO 12100 risk-reduction process. Signed FAT/SAT checklist, updated risk assessment, as-built electrical drawings, operating instructions, training records, and validation log. Every safety function passes documented tests at installation, after safety-related changes, and at the intervals defined by the risk assessment and site procedures.
Important: PL d and Category 3 are design targets for safety-related control systems, not a substitute for a complete machine risk assessment. Final guard dimensions, safety distances, stopping performance, validation intervals, and legal compliance requirements must be determined for the specific cell and installation conditions.

Model OEE, Labor Savings, and a Payback Target Below 24 Months

Buying an automated welding cell requires more than checking torch reach and quoted cycle time. Measure current output, weld time, changeover losses, rework, and unplanned downtime. These figures create a practical OEE baseline. Availability, performance, and quality must be modeled separately. A cell running quickly can still lose money through fixture delays or weld defects. Request a live trial with representative parts, joint types, and realistic material handling.

Labor savings need careful definition. Count direct welding hours, inspection time, loading, unloading, and maintenance support. Do not assume every saved hour becomes an immediate payroll reduction. Skilled workers may move to programming, quality checks, or additional cells. Include training, guarding, integration, tooling, spare parts, energy, and planned maintenance in the business case. Our early estimates were too optimistic because changeovers took longer than expected.

Set a payback target below 24 months, then test it against conservative assumptions. Use this formula: total investment divided by monthly net savings. Model several production volumes, including a slow month. Add scrap reduction only when reliable quality records support it. Ask for downtime data, acceptance criteria, service response times, and operator training details. A spreadsheet should show the impact of one extra shift, a five-percent OEE decline, and delayed production. If the payback disappears under modest pressure, the project needs better evidence, not stronger sales language.